SMT Solder Paste Manufacturers.

Focused on SMT soldering processes, a one-stop electronic soldering solutions provider.

Here you can find knowledge about Solder Bar Manufacturer, including but not limited to usage methods, installation techniques, troubleshooting and more. Focused on SMT soldering processes. If you can't find what you need, please contact us anytime.
The sphericity, particle size distribution, and oxidation level of tin powder particles in SAC solder paste directly affect the release integrity and pad coverage during solder paste printing. Actual production lines have found that spherical tin powder with a D50 of 25μm can achieve a release rate of over 92% on a 38μm aperture stencil. When the D50 deviation exceeds ±1.5μm or the oxygen content is >0.5wt%, the defect rates of solder bridging and insufficient solder increase by more than 3 times. The process compatibility of solder paste, SAC solder paste, and tin powder solder paste must be based on measured particle parameters.
Published: 2018-04-13During PCB pad processing, the soldering performance of ENIG, Immersion Silver and OSP processes differs significantly. The ENIG layer is oxidation-resistant but has poor wettability, requiring high-activity solder paste. Immersion Silver is prone to sulfidation discoloration and sensitive to reflow peak temperature. Uneven OSP film thickness can cause local non-wetting. The three processes must be managed differentially in stencil aperture design, reflow profile setting, and incoming material storage conditions.
Published: 2018-04-13
Opening the solder paste container directly without sufficient warm-up will cause abnormal increase in solder paste viscosity, uneven flux precipitation, poor printing release, and increased void rate of solder joints. In severe cases, it will lead to batch defects such as solder bridging, insufficient solder, and cold solder joints. The warm-up of solder paste must strictly follow the requirement of standing at room temperature for 2 to 4 hours. Before opening the solder paste, it is necessary to confirm that the warm-up is sufficient and there is no condensed water on the surface.
Published: 2018-03-26During the pin dip soldering process, oxidation of the solder bath surface is the main cause of continuous dross generation. Jiajinyuan anti-oxidation flux, through the synergistic effect of dynamic coverage and active ingredients, forms a dense inert film on the solder bath surface, reducing the oxidation rate by more than 70% during pin dip soldering, cutting daily dross production by 1.2kg, significantly extending the cleaning cycle of the solder pot, and stabilizing solder joint wettability.
Published: 2018-03-2401005 packaged components, with their extremely small pad dimensions and narrow solder paste volume tolerance, are a high-incidence area for solder beads. Residual solder beads can easily cause creeping discharge and breakdown during high-voltage testing, directly threatening the insulation reliability of products. Production line data from Jiajinyuan shows that this type of defect accounts for 68.3% of the total solder bead incidence, requiring coordinated control from three aspects: stencil aperture design, squeegee pressure, and reflow atmosphere.
Published: 2018-02-20To address persistent issues such as uneven solder paste deposition, cold soldering, and solder bridging during thick copper foil soldering on multilayer boards, this paper draws on 20 years of measured data from Jia Jinyuan's production lines, focuses on precise solder paste dosage control methods, and details the matching logic for thick copper solder paste printing parameters, covering key actions such as stencil aperture design, squeegee pressure and speed coordination, and SPI detection threshold setting before reflow soldering.
Published: 2018-02-09Cold soldering is one of the most stubborn soldering defects in SMT production of large thick copper boards, occurring frequently especially on PCBs with copper thickness ≥2oz and dimensions ≥400mm×300mm. The root cause is that the large heat capacity of the copper substrate and delayed temperature rise lead to insufficient solder paste reflow. In production line tests, Jiajinyuan cold soldering repair paste can reduce the cold soldering defect rate from 1.8% to below 0.3%.
Published: 2018-02-07The standard for solder paste warm-up directly determines printing accuracy and solder joint reliability. Insufficient warm-up will lead to typical soldering defects such as high solder paste viscosity, poor demolding, solder paste collapse, and cold solder joints. Solder paste must strictly follow the 4-hour room temperature warm-up specification before use to avoid batch SMT defects caused by rushed production line launch.
Published: 2018-01-30Connector solder must balance wettability, residue control, and thermal shock resistance. Jia Jinyuan solder wires and bars can achieve capillary filling within 0.3 seconds in terminal dip soldering, maintain a bridging rate below 0.08% at an automatic soldering track speed of 1.2 m/min, and meet the dual-mode soldering requirements of 0.5mm-pitch FPC connectors and IDC crimp terminals.
Published: 2018-01-17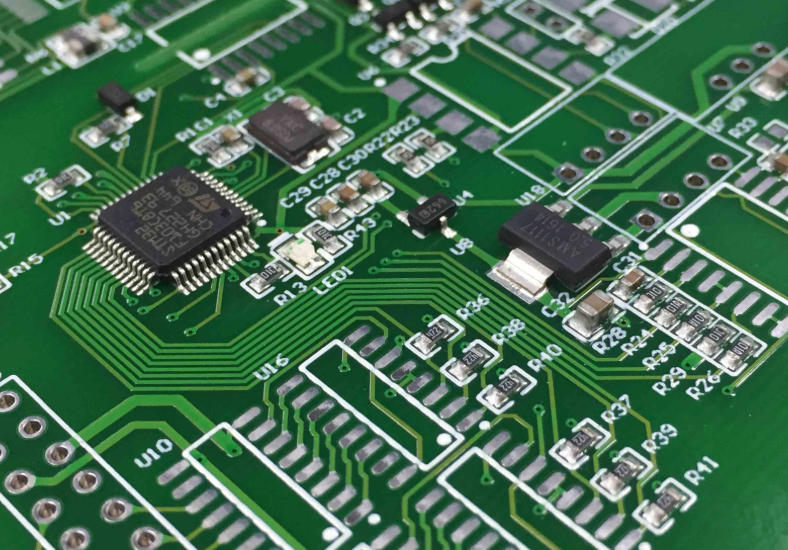
The solder paste itself is non-conductive; its metallic components are encapsulated by rosin or resin and remain in an insulating state when not melted. However, before reflow soldering, excessive residue, printing misalignment, or incomplete cleaning may still cause circuit short circuits due to ionic residue or solder bead bridging. In actual production lines, over 85% of short circuit problems stem from process control failures rather than the intrinsic conductivity of the solder paste.
Published: 2018-01-14Our technical team is always ready to provide professional solder material selection advice and SMT process solutions.