SMT Solder Paste Manufacturers.

Focused on SMT soldering processes, a one-stop electronic soldering solutions provider.

Here you can find knowledge about Solder Paste Wholesale, including but not limited to usage methods, installation techniques, troubleshooting and more. Focused on SMT soldering processes. If you can't find what you need, please contact us anytime.
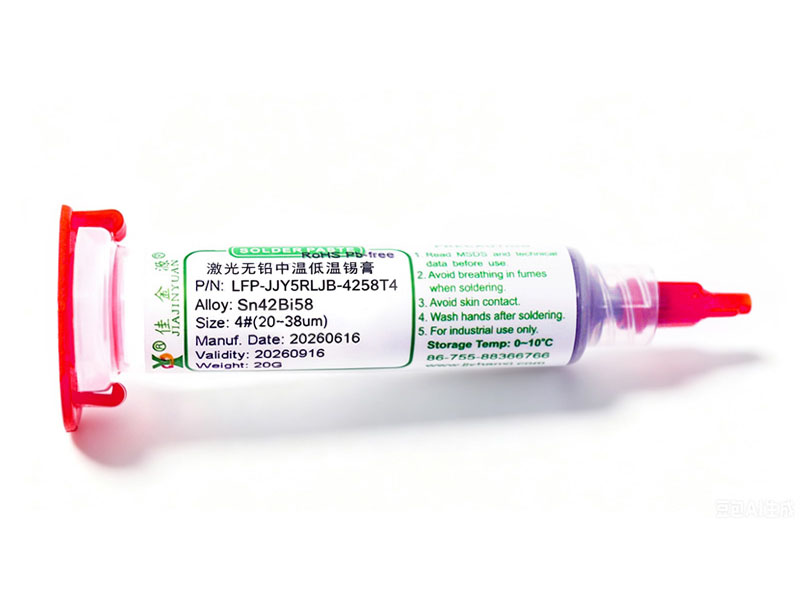
LFP?5RLJ?0307 laser high-temperature solder paste is specifically designed for jet valve laser welding, featuring high activity and low residue. It is suitable for precision dispensing scenarios such as pneumatic valves and screw valves. Its halogen-free formula and stable alloy powder ensure no solder beads during the welding process, improving process reliability and product yield.
Published: 2026-08-28
Domestic halogen-free solder paste LFP?5RQ?0307 achieves nearly 100% solder wetting in QFN packages, with its high activity and alloy powder characteristics being the key factors. Optimizing printing parameters and reflow profile can further improve soldering quality.
Published: 2026-08-28
In SMT manual rework soldering scenarios, the choice between rosin-core solder wire and solid-core solder wire must be closely tied to solder joint quality, operational efficiency, and rework risk. Rosin-core solder wire is suitable for rapid rework soldering of small-batch, high-density, low-heat-capacity components, while solid-core solder wire is more appropriate for large pads, high-heat-capacity components, and military or medical PCBA sensitive to residues. The two have essential differences in terms of flux activity, thermal response, cleanability, and cost.
Published: 2026-08-27
Low-residue solder paste is a key material for enabling SMT no-clean processes. It can control ionic residues below 10.06μg/cm2 NaCl equivalent after reflow soldering, avoiding leakage, corrosion, and CAF failures caused by rosin or organic acid residues. It is especially suitable for high-density, fine-pitch automotive-grade and medical electronics assembly without underfill.
Published: 2026-08-27
The QFN void rate standard is tightening from the 25% limit in IPC-A-610 Revision G to the automotive-grade 5% requirement. The void-reduction capability of solder paste has become a dividing line for mass production yield. Low-residue, high-thixotropy, and gradient-evaporation solder pastes are rapidly replacing traditional formulations. Combined with a nitrogen atmosphere and optimized reflow profiles, this enables a systematic reduction in void rates.
Published: 2026-08-27
The formation causes of wave soldering dross involve the purity of solder bars, oxide film control, and the synergistic imbalance of process parameters. By comparing the dross generation amount of high-purity solder bars and conventional solder bars under different chain speeds, wave heights, and nitrogen protection, combined with the actual line changeover cost and maintenance frequency of the production line, the two-way optimization path of the solder bar process is clarified, providing a feasible selection basis for the mass production of high-reliability PCBs.
Published: 2026-08-27
The shelf life of solder paste and SMT material control are currently facing three major trends: the popularization of low-temperature storage, strengthened batch traceability, and compressed open-container usage timelines. The driving factors include the deepening of lead-free processes, growth in automotive-grade orders, and stricter customer audits. Industry impacts are reflected in increased fluctuation of scrap rates, higher line changeover frequency, and more IQC inspection items. Practitioners need to incorporate solder paste from warehousing to temperature recovery into MES control nodes throughout the entire process, and work backward from the actual production line takt to determine the open-container usage window.
Published: 2026-08-27
New energy circuit boards have extremely high requirements for soldering reliability; even a slight deviation in the selection of solder paste and solder wire can cause batch defects such as cold solder joints, bridging, and excessive voiding rates. Combined with real production line failure cases, this article directly addresses core pain points such as insufficient solder paste activity matching, mismatched silver content in solder wire, and lack of coordination between reflow profile and solder paste melting point, and provides immediately executable material verification processes and parameter locking methods.
Published: 2026-08-27
Sn63Pb37 solder paste still has irreplaceable process stability in through-hole SMT production lines. Its eutectic properties bring low melting point, narrow reflow window and excellent wettability. However, limited by RoHS compliance pressure and lead-free mixed line risks, practical applications must directly address high-frequency failures such as solder joint cracking, cold solder joints, insufficient wetting, and stencil clogging, which are particularly evident in 0201 component soldering and double-sided board rework scenarios.
Published: 2026-08-27
There are significant differences between SMT nitrogen soldering and air soldering in terms of solder paste wettability, void rate, solder joint finish, and flux residue performance in actual production lines. Nitrogen soldering can reduce the void rate of BGA solder joints from 15%~25% in air soldering to 3%~8%, with particularly prominent advantages on OSP copper surfaces, fine-pitch QFNs, and high-reliability military boards, but the cost of nitrogen consumption and equipment compatibility must be weighed.
Published: 2026-08-27Our technical team is always ready to provide professional solder material selection advice and SMT process solutions.